21×10 / 22×12 Forged Monoblock Wheels for 2025 Chevrolet Corvette Z06 (C8) – Gloss Black Ten-Spoke Staggered 5×120
- Model: 26-10-06-06-04 (JC135H / JC172)
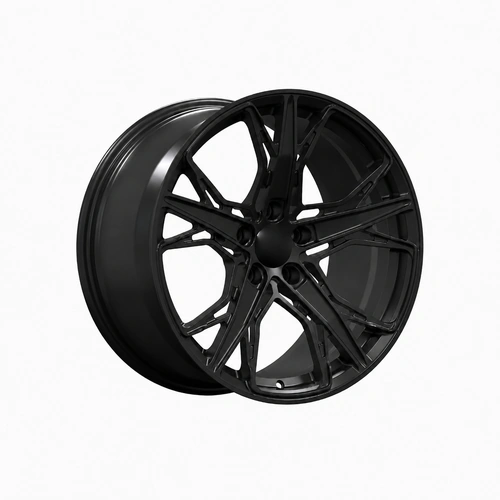
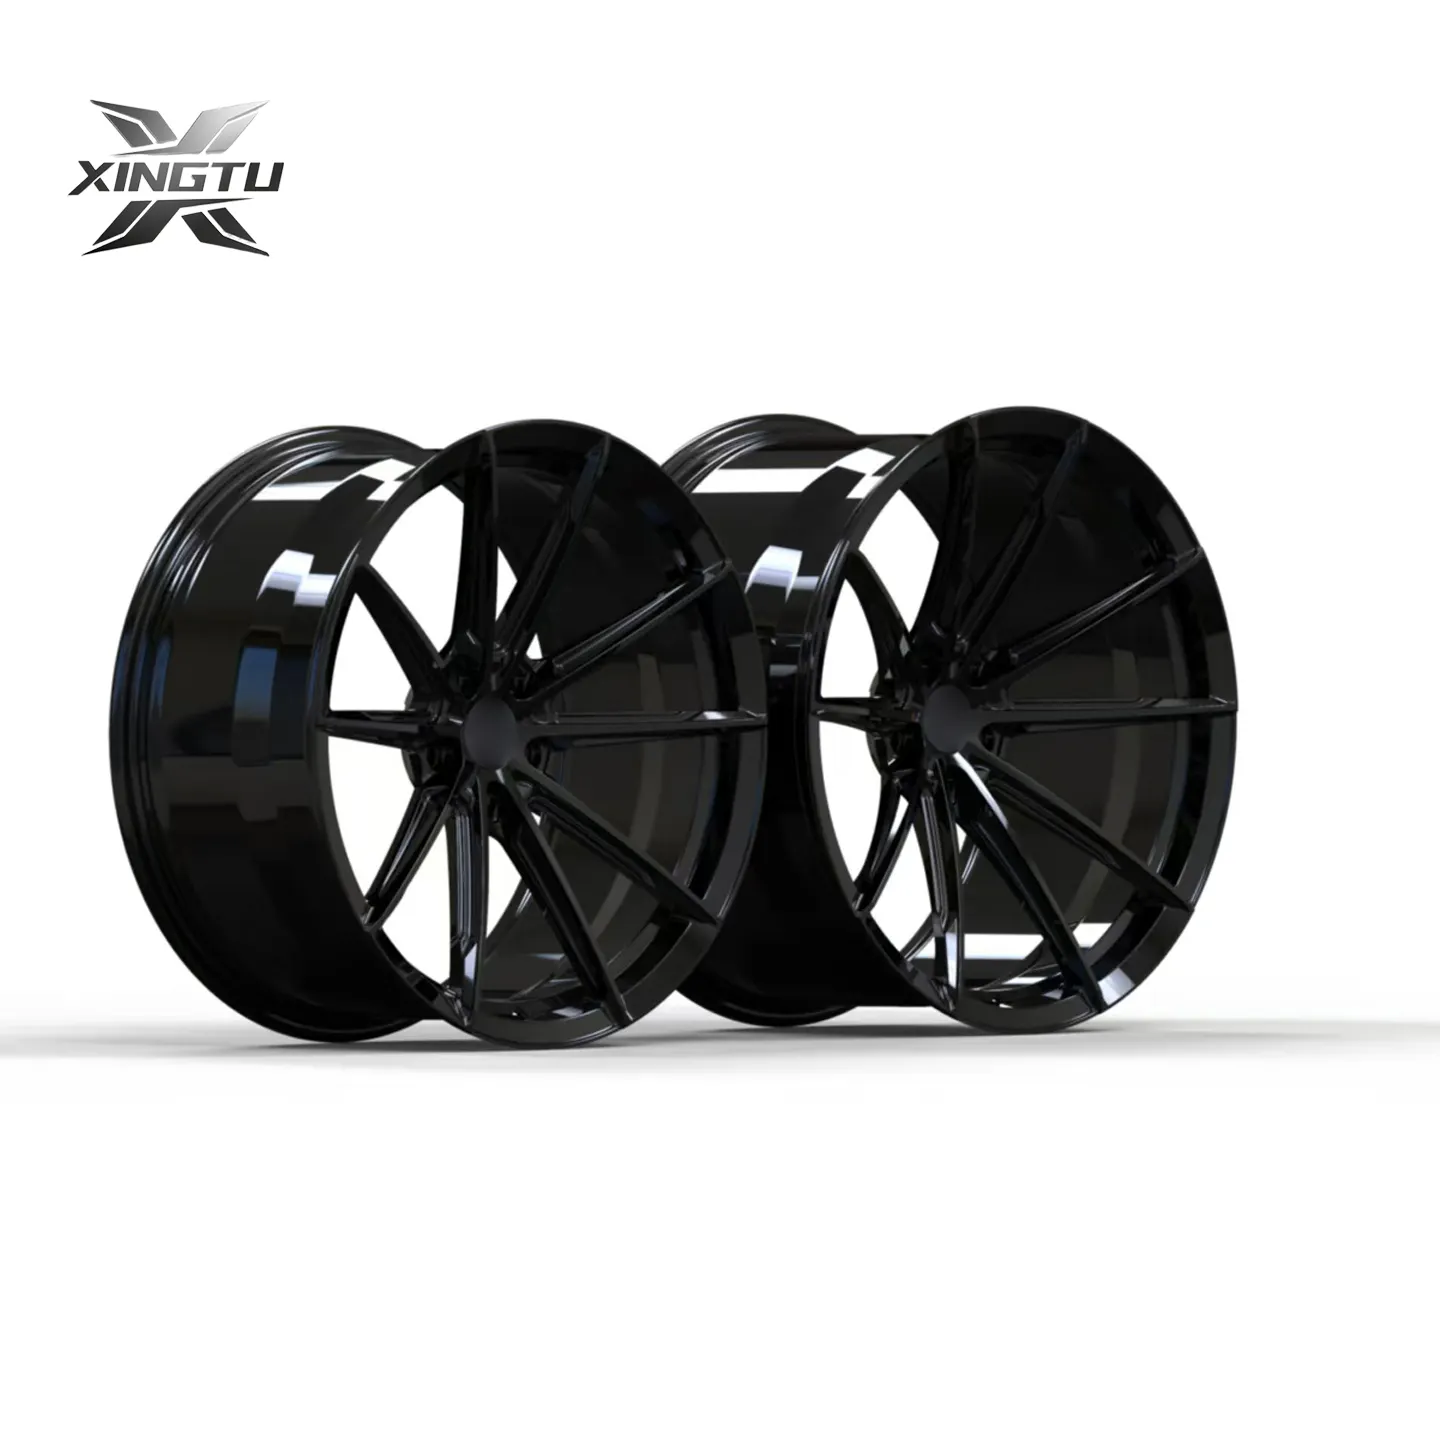
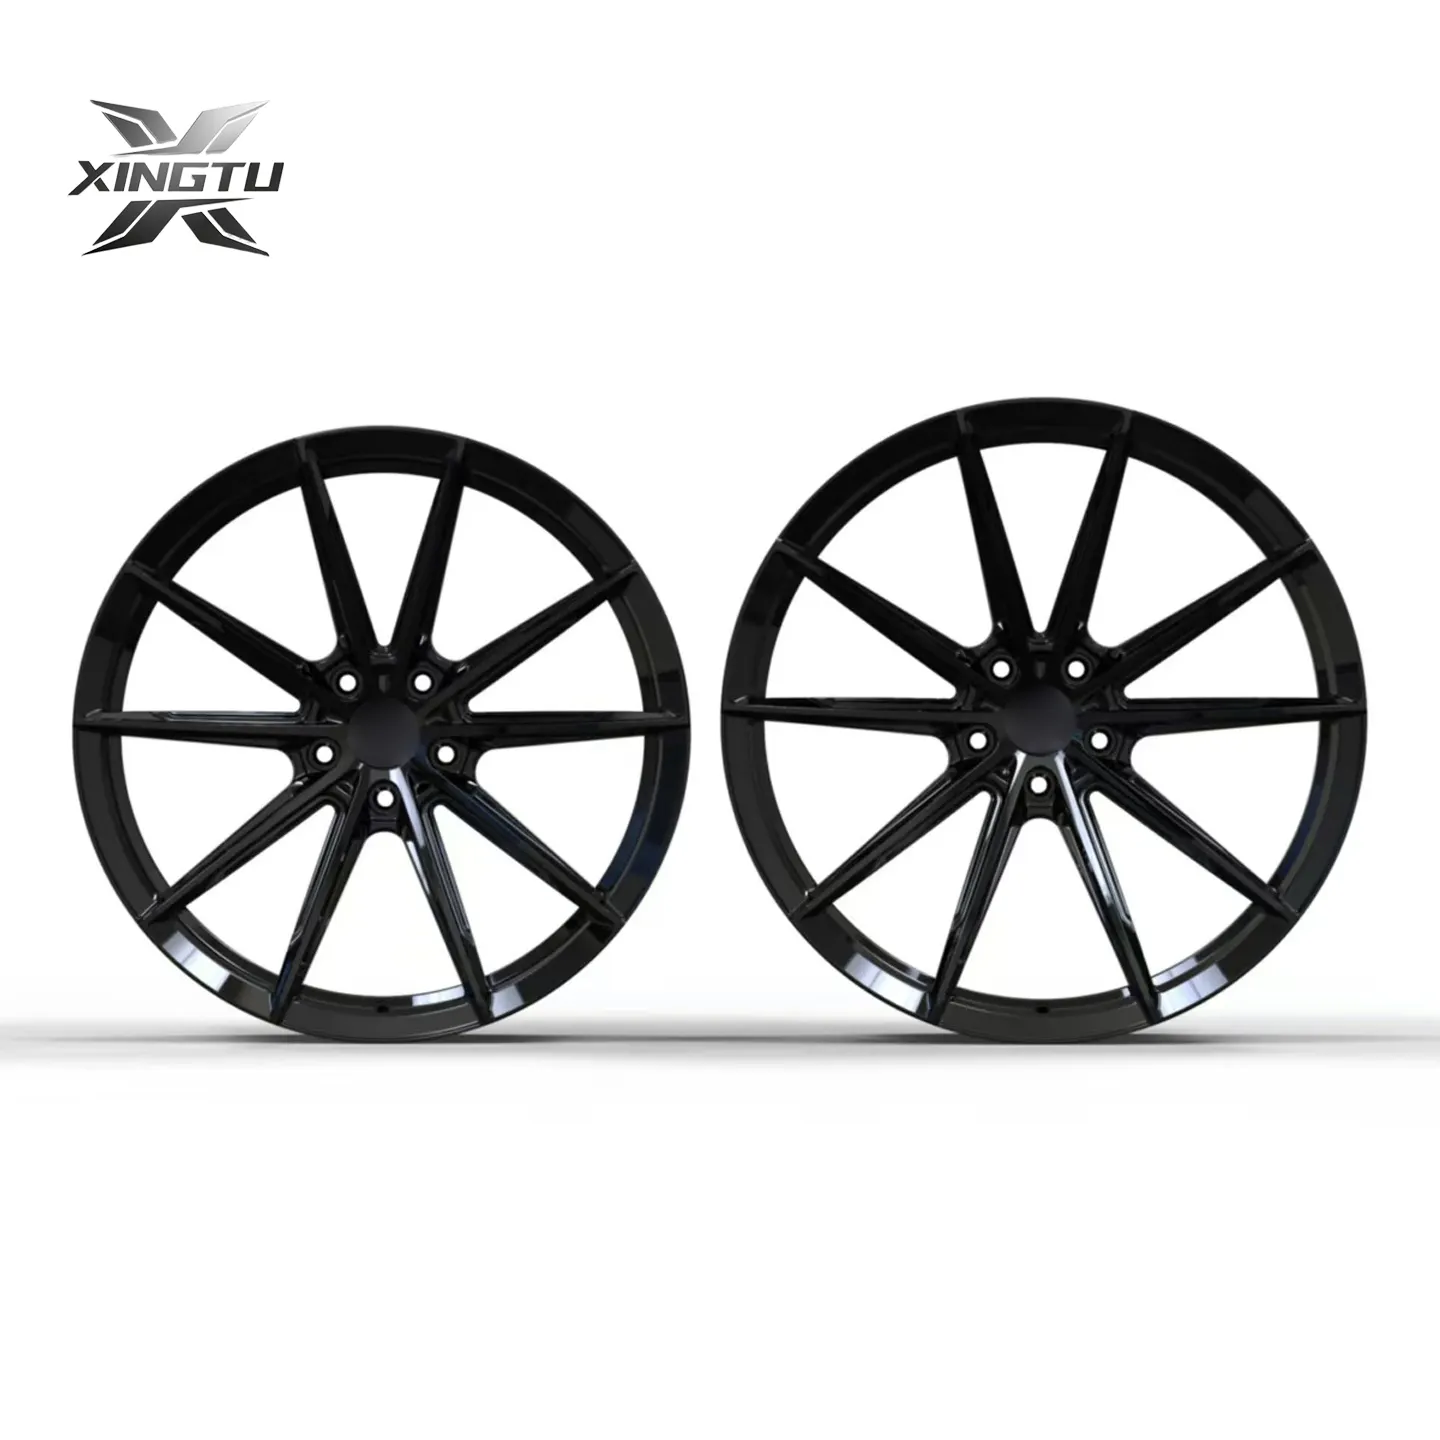
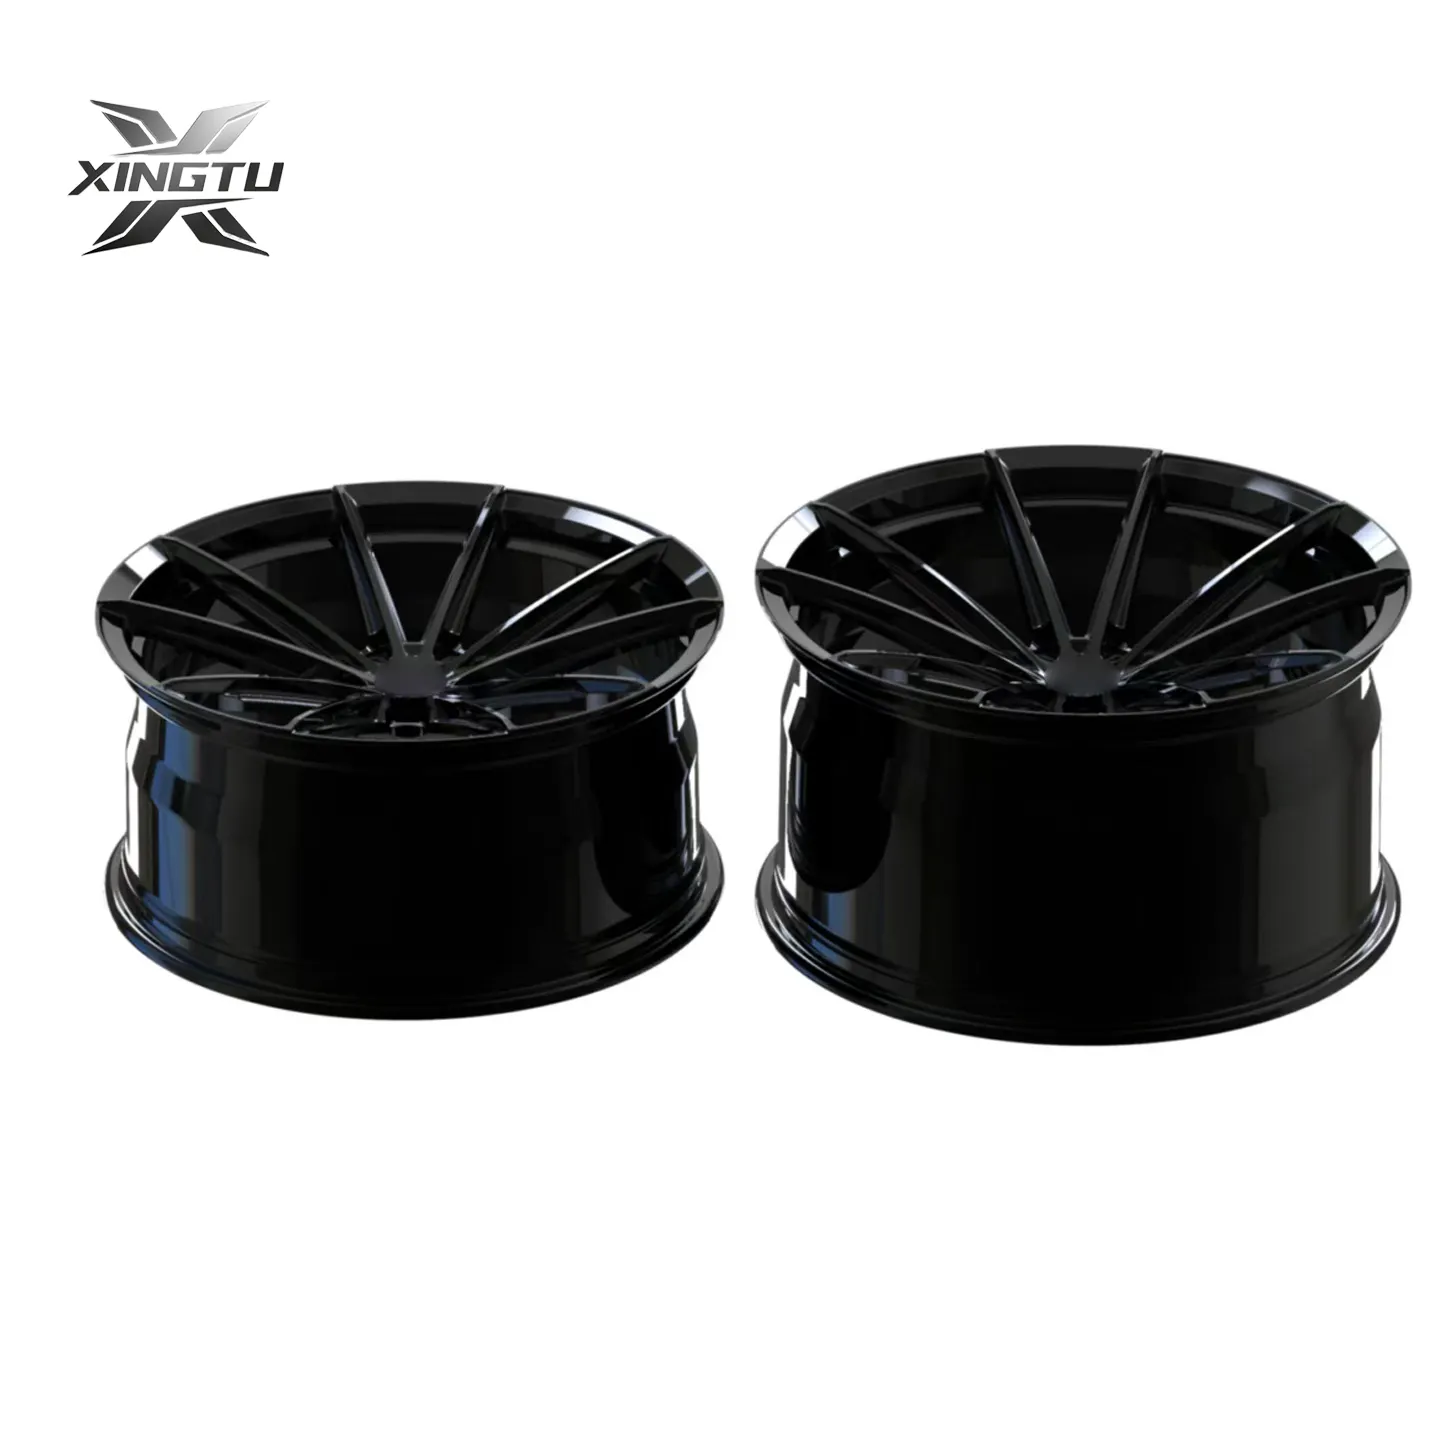
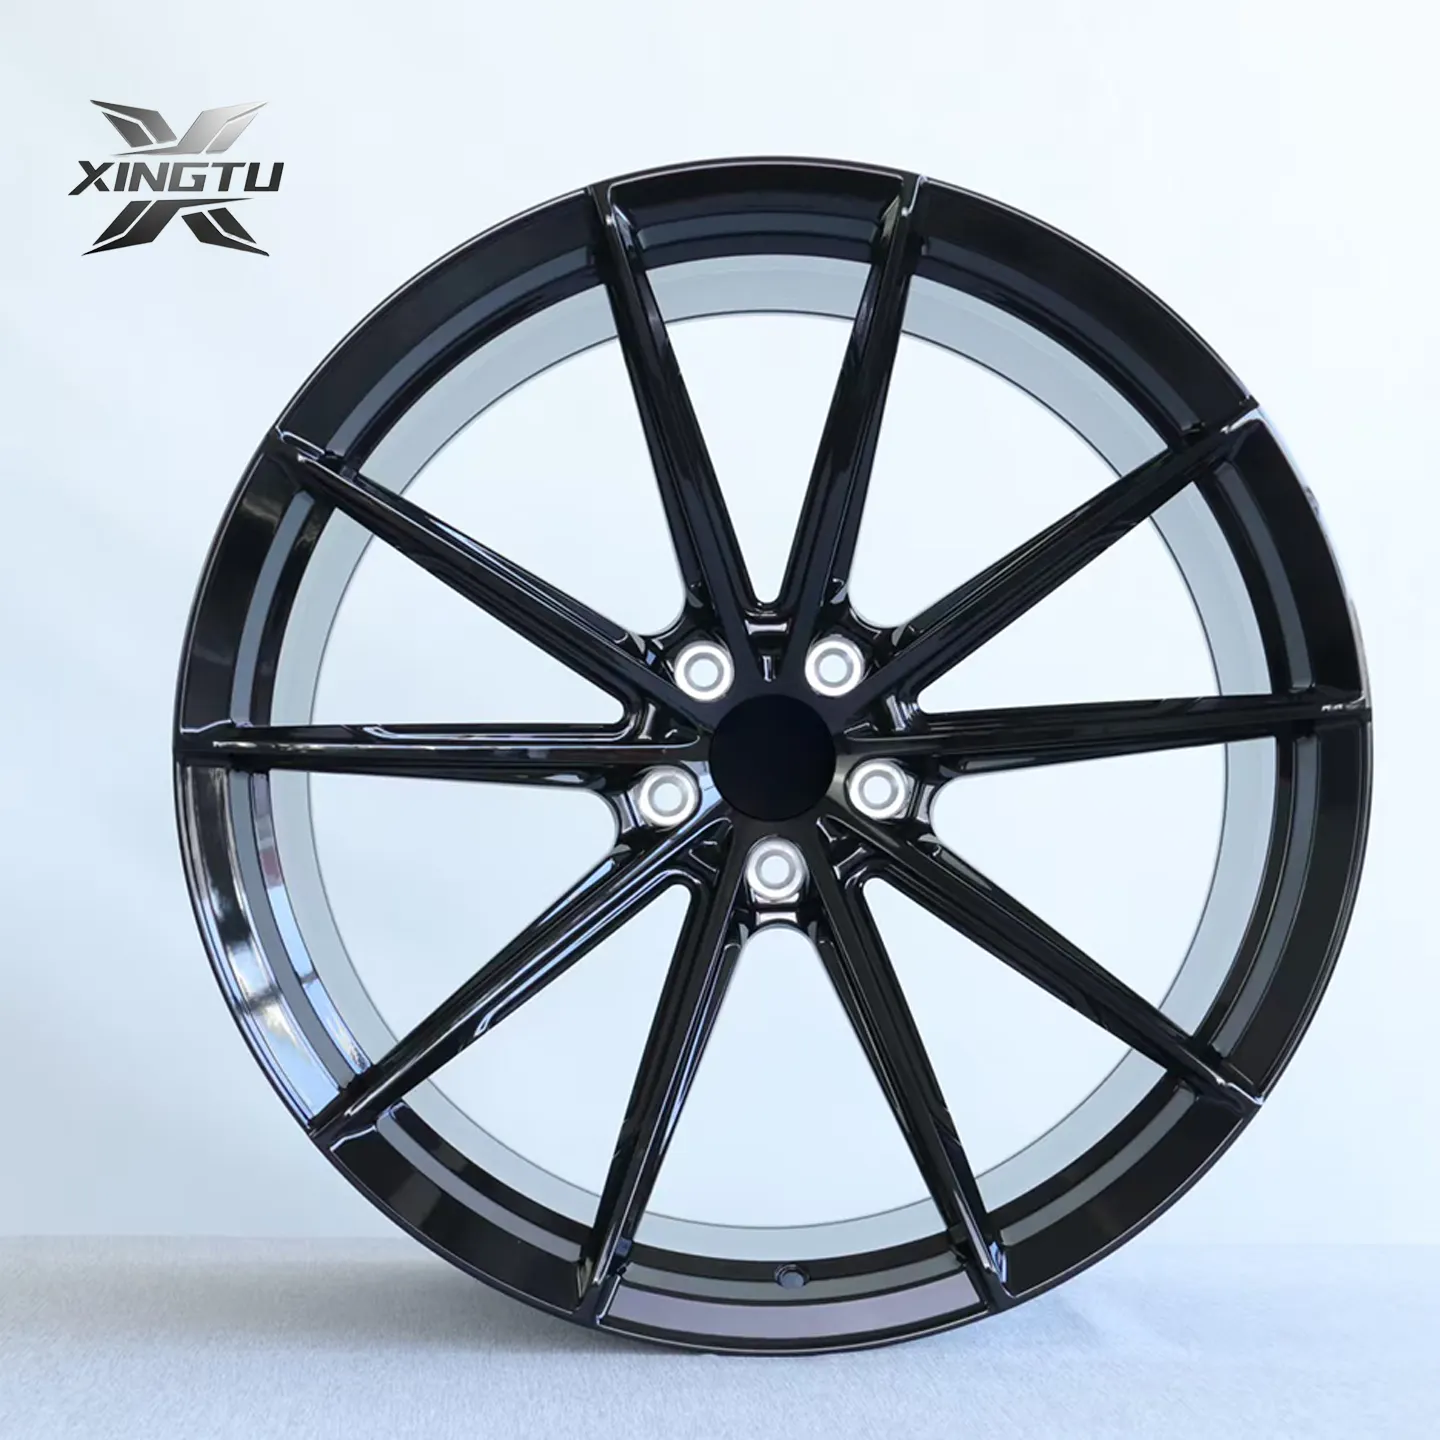
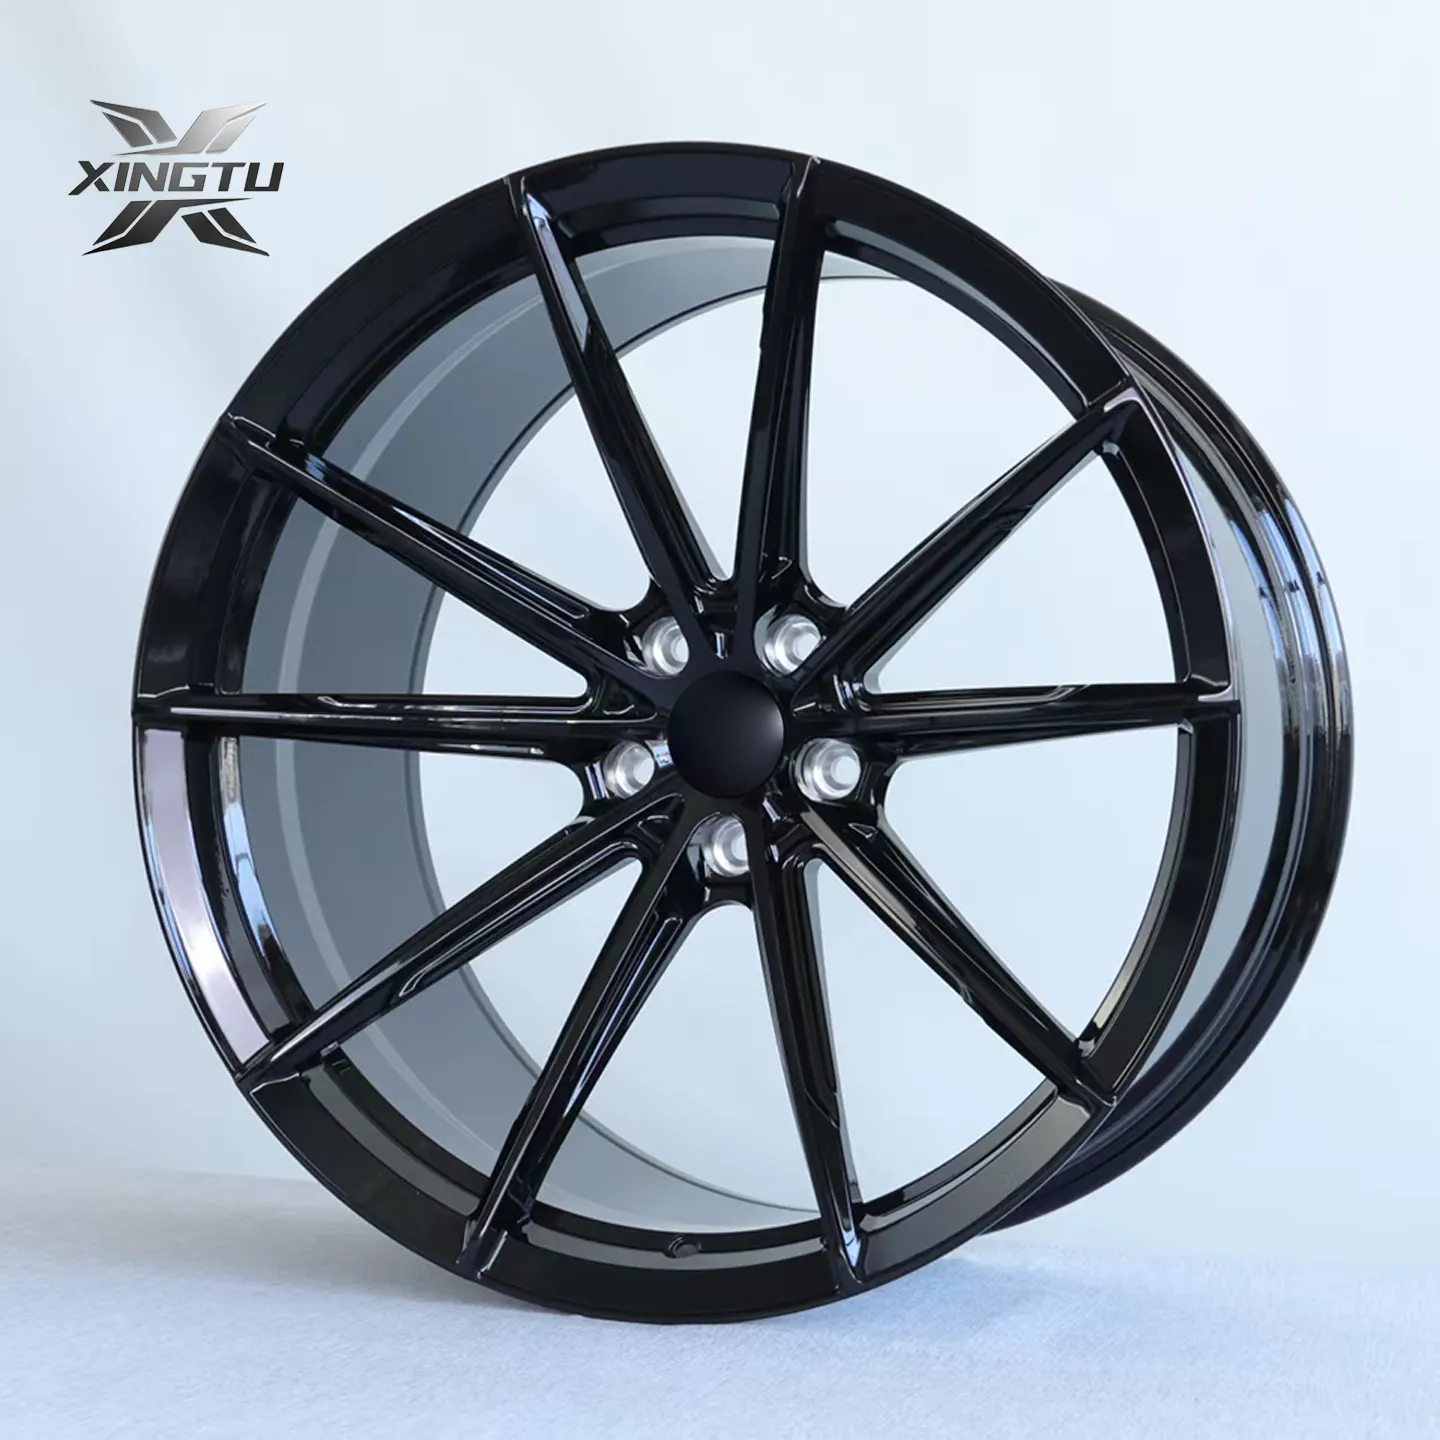
Developed for a 2025 Chevrolet Corvette Z06, this staggered forged set moves to 21×10.0 ET22 at the front and 22×12.0 ET20 at the rear. Each wheel is cut from a single forged blank, with five pairs of slim spokes shaped deep enough to carry load without giving the face unnecessary visual weight. The finished wheels weigh 12.4 kg and 13.9 kg respectively and carry a 960 kg load rating per wheel. A full gloss black finish draws the face, lip and barrel into one compact form while reflected light picks out the spoke edges and deep windows.



Specifications
| Item | Specification |
| Model No. |
26-10-06-06-04 (JC135H / JC172) |
| Size |
Front: 21×10.0 Rear: 22×12.0 |
| PCD |
5×120 |
| Offset (ET) |
ET22/20 |
| Center Bore |
66.9 mm |
| Weight |
12.4/13.9 kg per wheel |
| Load Rating |
960 kg per wheel |
| Lug Seat |
15×32 60° taper |
| Finish |
Gloss Black (full paint) |
| Construction | Forged Monoblock |
| Fitment Basis | Check Data |
| Lead Time |
25 days (brushed finish) |
-
Descriptions

A Larger Diameter Without Losing the C8 Proportion
The 21/22-inch combination is a plus-one change on both axles compared with the original 20/21-inch Z06 arrangement. That extra diameter had to work with the car's wide rear body rather than simply make the rear wheel appear larger. A 21×10.0 ET22 front and 22×12.0 ET20 rear specification gives the set a deliberate front-to-rear progression, while the rear remains one inch narrower than the factory rear wheel.
Mounting geometry follows the submitted project data: 5×120 PCD, 66.9 mm center bore and a 15×32 60° taper seat. Conical-seat hardware is required; ball-seat nuts are not interchangeable. Because this is a non-standard wheel and tire package, carbon-ceramic brake clearance, suspension and liner clearance, the rear fender relationship and the selected tire section must all be checked on the actual car before fitment is approved.
Paired Spokes Carry the Load Through Depth
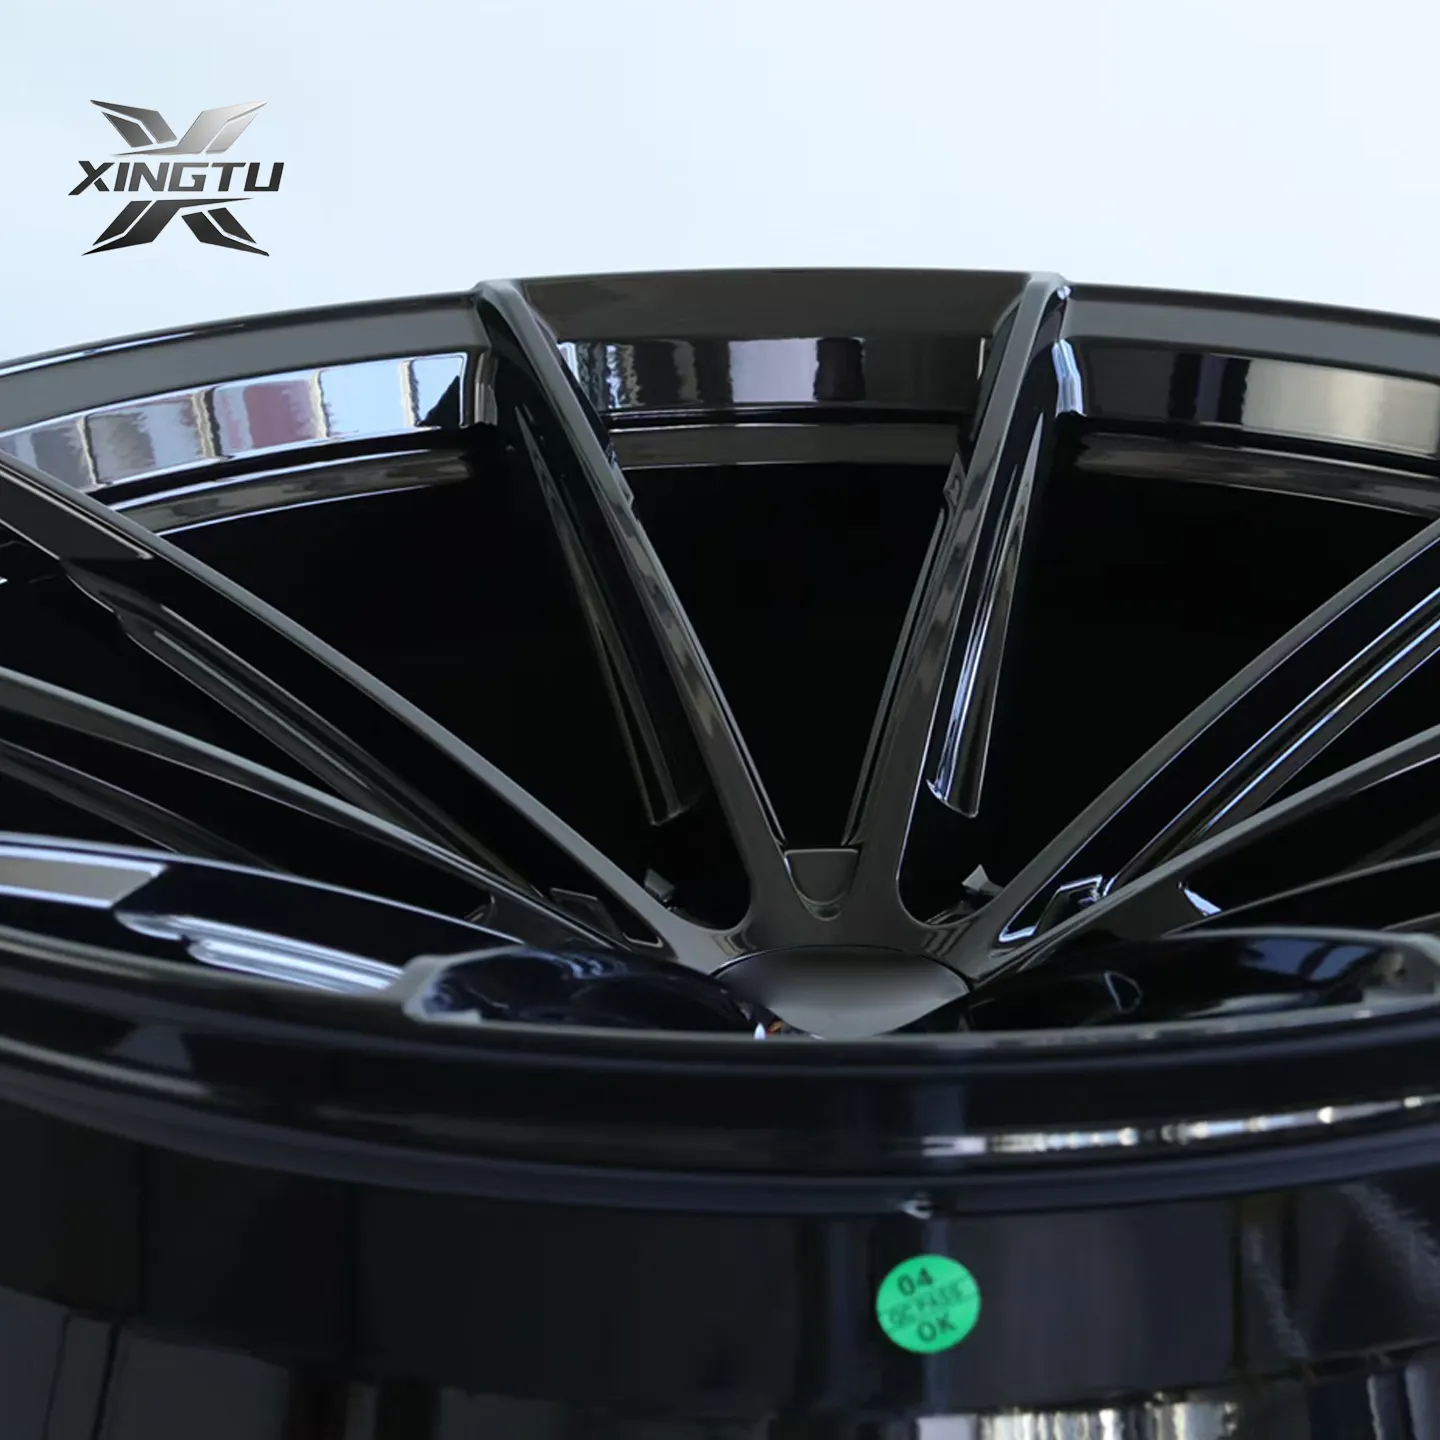
The ten-spoke face is machined as five closely related pairs. From the front, each spoke appears narrow and crisp. In section, however, the spokes gain depth from the hub pad toward the rim and meet their neighbors near the outer edge. This creates a direct load path without making the face look heavy.
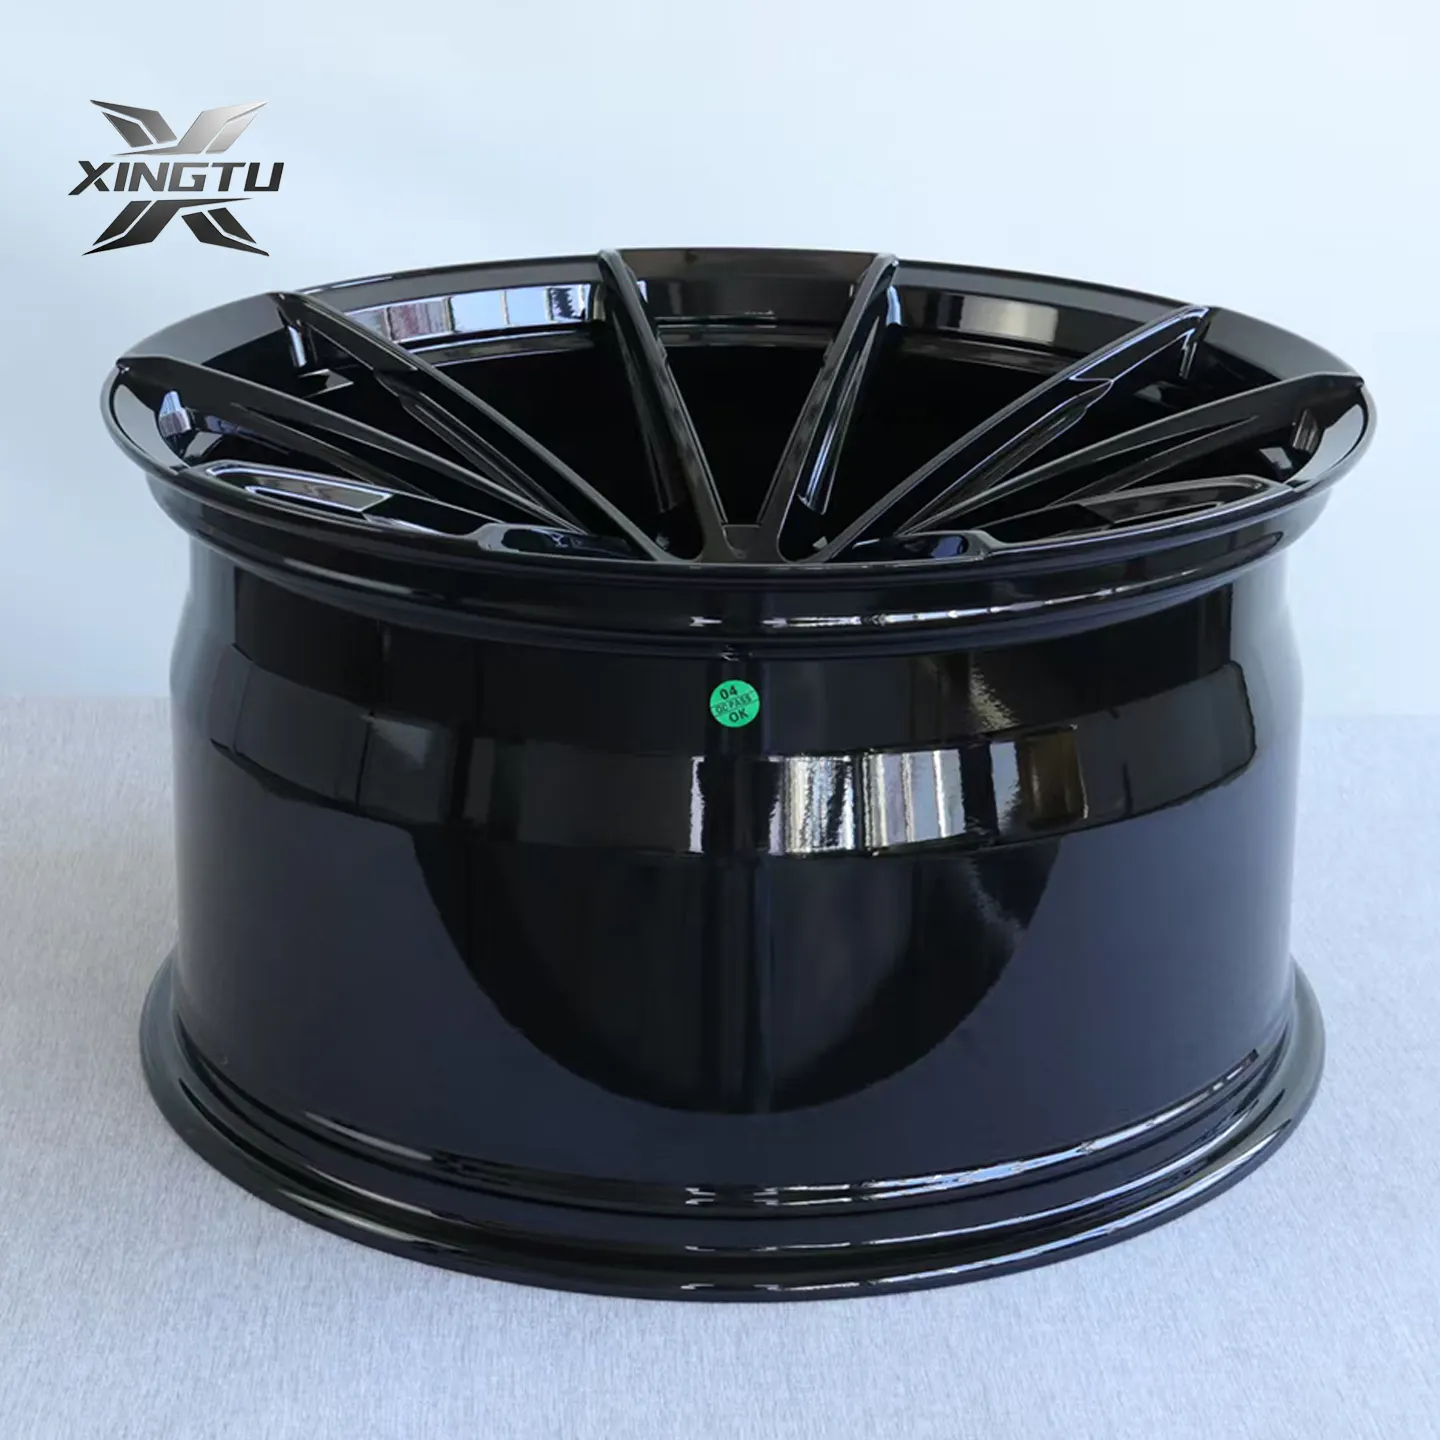
The front wheel finishes at 12.4 kg and the wider rear at 13.9 kg, with a 960 kg rating per wheel. Face, hub pad and barrel remain one continuous forged structure. The stepped lip is machined into that same blank for visual definition; it is not a separate rim section or a beadlock component.
Gloss Black Makes Surface Control Visible
On a wheel with narrow spokes and deep windows, gloss black is unforgiving. Paint must reach the spoke roots and inside corners without bridging the openings or building a thick edge. Any sanding line, polishing swirl or orange peel becomes more noticeable once the clear coat reflects direct light.
For that reason, the face, spoke sides, window edges and barrel are prepared as distinct surface zones before the wheel is coated as a whole. The aim is an even gloss level from the front face through to the flange, with clean separation at every spoke edge. The center remains a plain disc for the customer's cap; no third-party emblem is applied during production.
From Design to Delivery
Quality Verified
- Front 21×10.0 and rear 22×12.0 dimensions inspected
- ET22 front and ET20 rear offsets checked
- 5×120 PCD and 66.9 mm center bore verified
- 15×32 60° taper-seat interface checked
- Front weight verified at 12.4 kg and rear weight at 13.9 kg
- Load rating confirmed at 960 kg per wheel
- Paired-spoke geometry, root radii and outer junctions inspected
- Stepped lip and flange profile checked
- Gloss level and coating thickness inspected across face, windows and barrel
- Spoke roots checked for paint bridging and heavy edge build
- Radial and lateral runout checked
- Every wheel dynamically balanced
Result
The finished set gives the C8 Z06 a sharper, more architectural face. Five spoke pairs converge tightly at the hub, open into deep windows and finish against a stepped outer lip. Gloss black keeps the 21/22-inch package visually controlled, while the spoke edges reveal the geometry whenever the light moves across the wheel.
The staggered diameter follows the car's rear-biased proportion without making the rear appear oversized. A 12.4 kg front and 13.9 kg rear wheel also keeps the mass closely matched to the different jobs of the two axles. The plain center disc leaves the final cap choice with the customer.
Upgrading a Mid-Engine Corvette to a Larger Staggered Set?
XINGTU develops forged monoblock, two-piece and three-piece wheels around the vehicle's hub data, brake package, suspension travel, tire plan and load target. Gloss, satin, brushed, polished and two-tone finishes can be specified to suit the intended character of the build.
-
Build & Fitment
Fitment and Load Specification
Front: 21×10.0 ET22. Rear: 22×12.0 ET20. The set uses a 5×120 bolt pattern, 66.9 mm center bore and 15×32 60° taper seat. Use only compatible conical-seat hardware; ball-seat nuts must not be fitted.
This is a plus-one diameter package on both axles, with a rear rim one inch narrower than the factory Z06 rear. Each wheel is rated at 960 kg. Before installation, verify carbon-ceramic brake clearance, suspension and inner-liner clearance, rear fender position and the actual mounted tire section on the vehicle.
Monoblock Structure and Spoke Geometry
The paired ten-spoke face, hub pad and barrel are machined from one forged aluminum blank with no bolted joint. Spoke depth provides the structural section while the narrow front profile keeps the face open. Finished weights are 12.4 kg front and 13.9 kg rear. The stepped lip is a cosmetic feature machined into the single forging, not a separate rim or beadlock ring.
Full Gloss Black Finish
Deep windows and tight spoke roots require controlled coating coverage. The face, spoke sides and barrel are prepared separately, then painted and clear-coated as one wheel to maintain a consistent gloss level. Inner corners are checked for bridging, and exposed edges are inspected for excessive film build. The center disc is left blank for a customer-supplied cap.
-
FAQs
1. Is this 21/22-inch set a universal direct fit for every C8 Z06?
No. The wheels were produced to the recorded project dimensions, but vehicle configuration and tire choice still affect clearance. Brake calipers, suspension, inner liners, fenders and mounted tire sections must be verified on the individual car.
2. Which lug-seat hardware does this wheel require?
The wheel uses a 15×32 60° taper seat and must be installed with compatible conical-seat hardware. Ball-seat nuts do not provide the correct contact surface and must not be substituted.
3. Why use deep paired spokes instead of thicker-looking spokes?
The spoke pairs gain structural section through depth rather than front-face width. This gives the wheel a clear, open appearance while supporting the published 960 kg rating.
4. Is the stepped lip a separate component?
No. The lip is machined into the same forged blank as the face and barrel. It adds visual depth but does not make the wheel two-piece or beadlock-equipped.
5. What makes the gloss black finish demanding on this design?
The narrow spoke roots and deep windows make even coating coverage difficult, while the reflective surface exposes sanding marks, edge build and orange peel. Surface preparation and coating flow are therefore checked closely across the entire wheel.
6. How long did this recorded build take?
The documented production schedule was 25 days from data review to final inspection and packing. Shipping time and any later design or fitment revisions are separate.
7. Is a branded center cap included?
The center is supplied as a plain disc for the customer's cap solution. No third-party emblem is installed at the factory.
Related Products