19×9.5 / 20×11 Forged Monoblock Wheels for Chevrolet Corvette Z06 (C5) – Hand-Brushed Finish with Transparent Protective Powder Coat 5×120.65
- Model: L266531 (blank: JC114 / JC023)
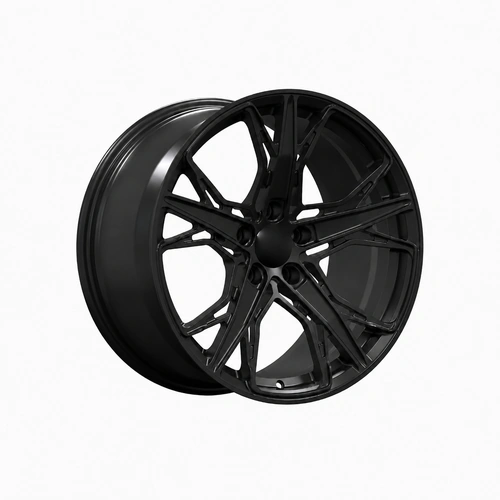
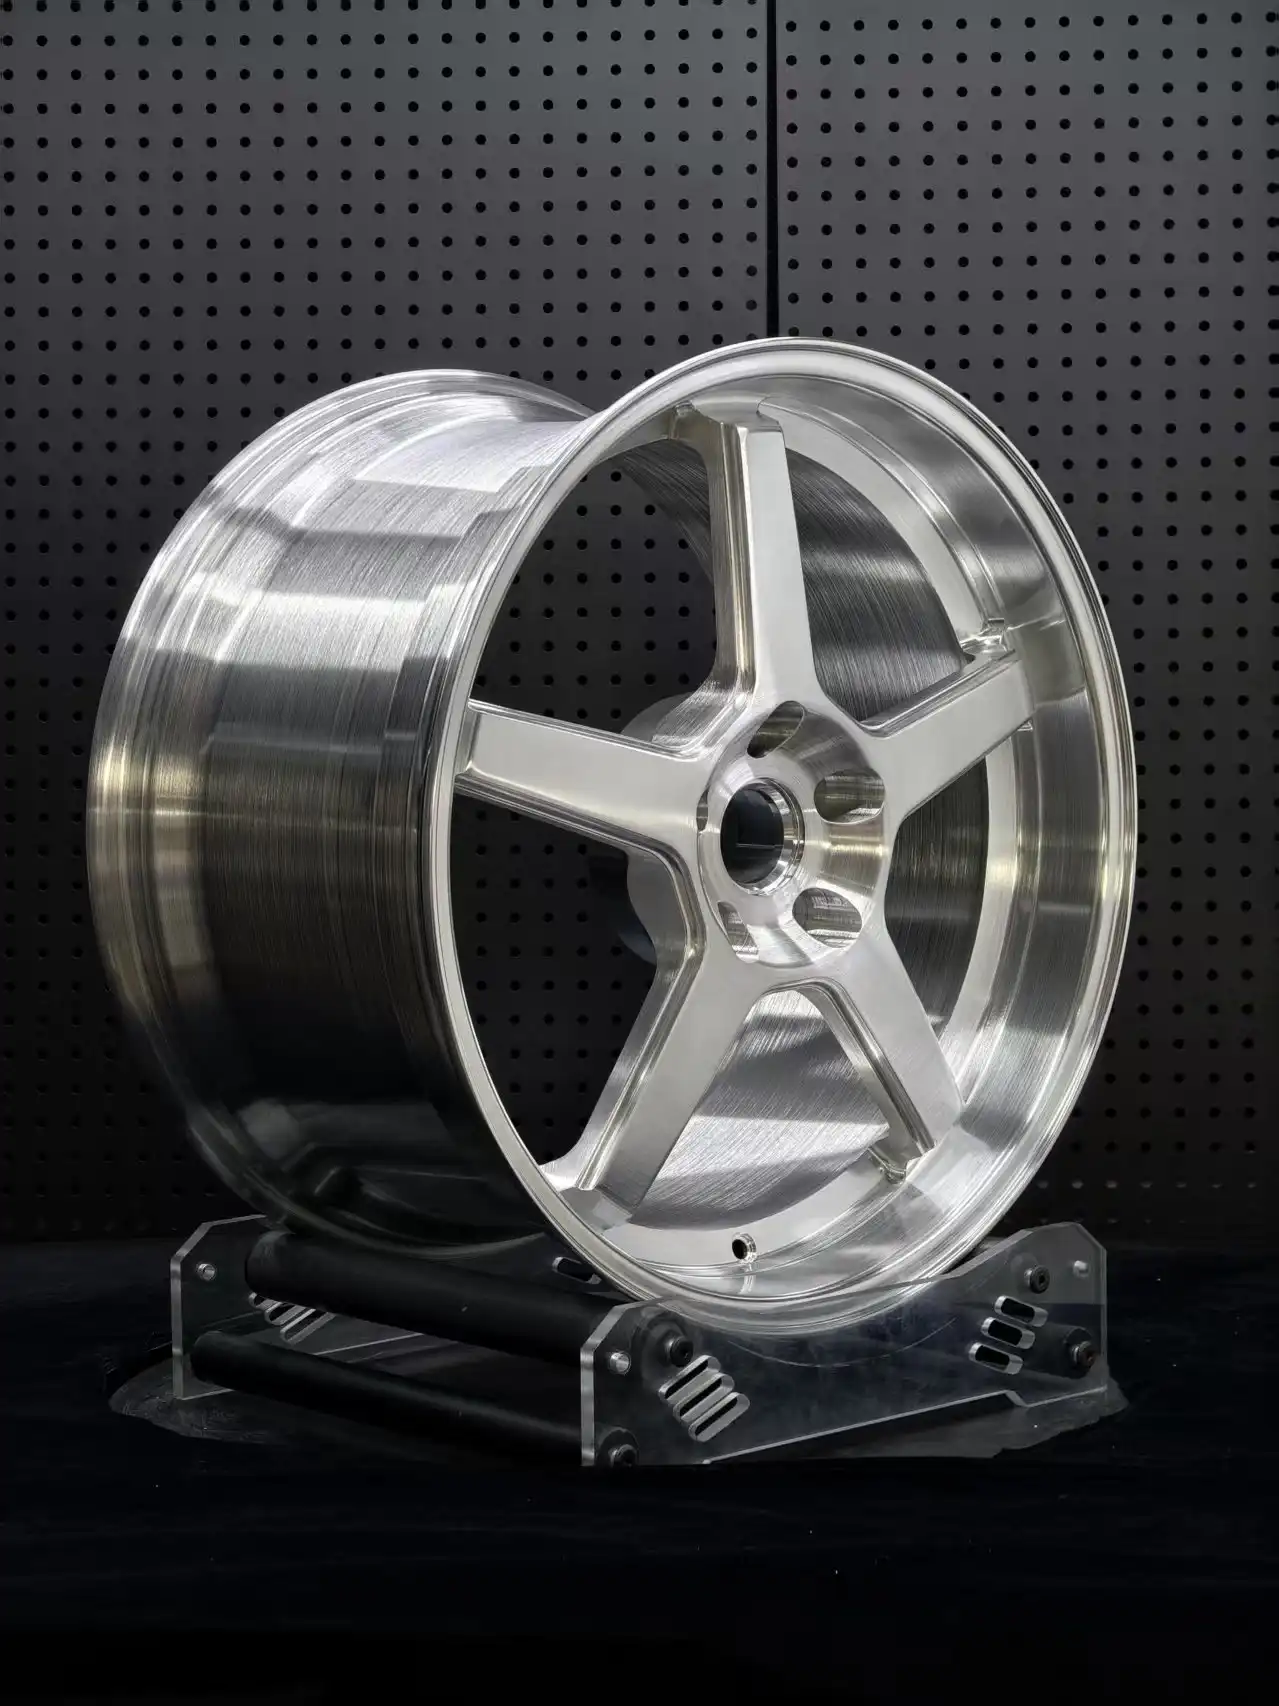
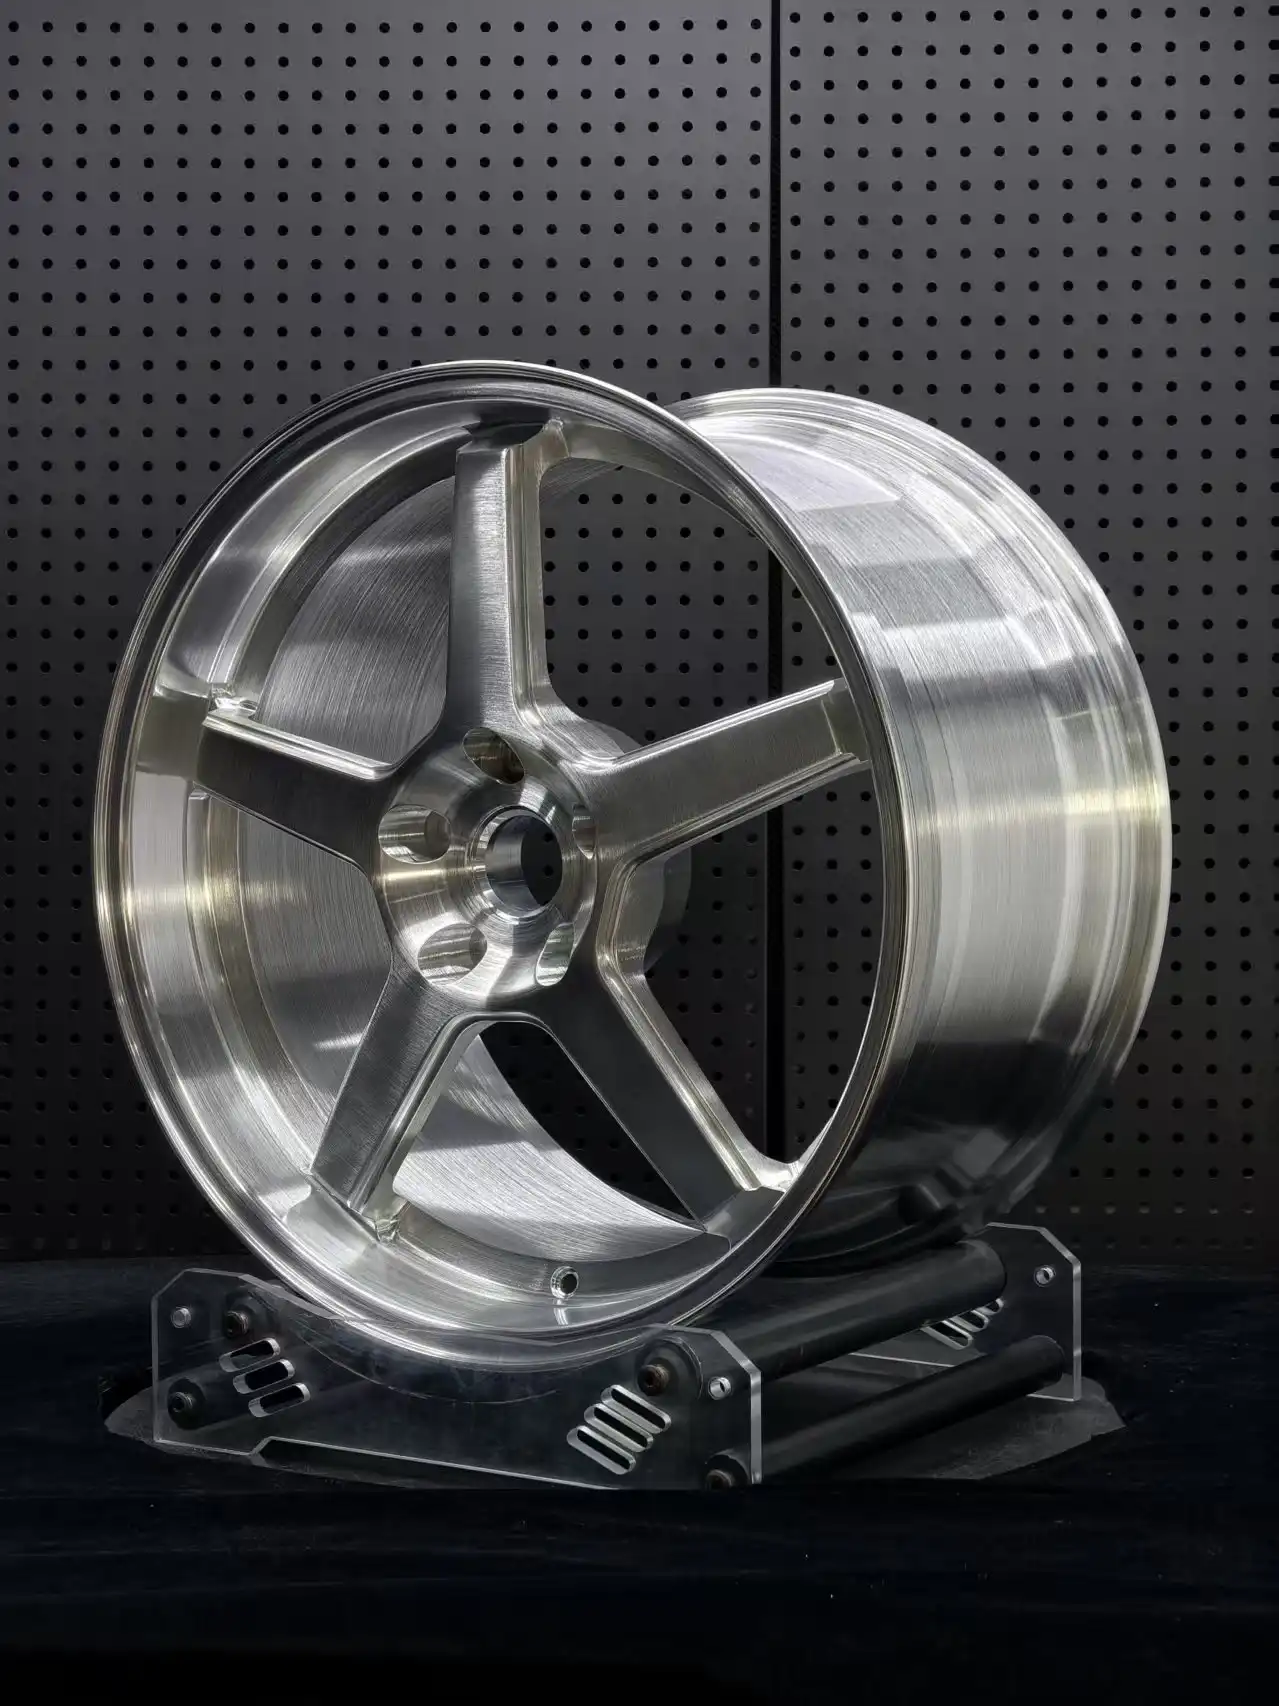
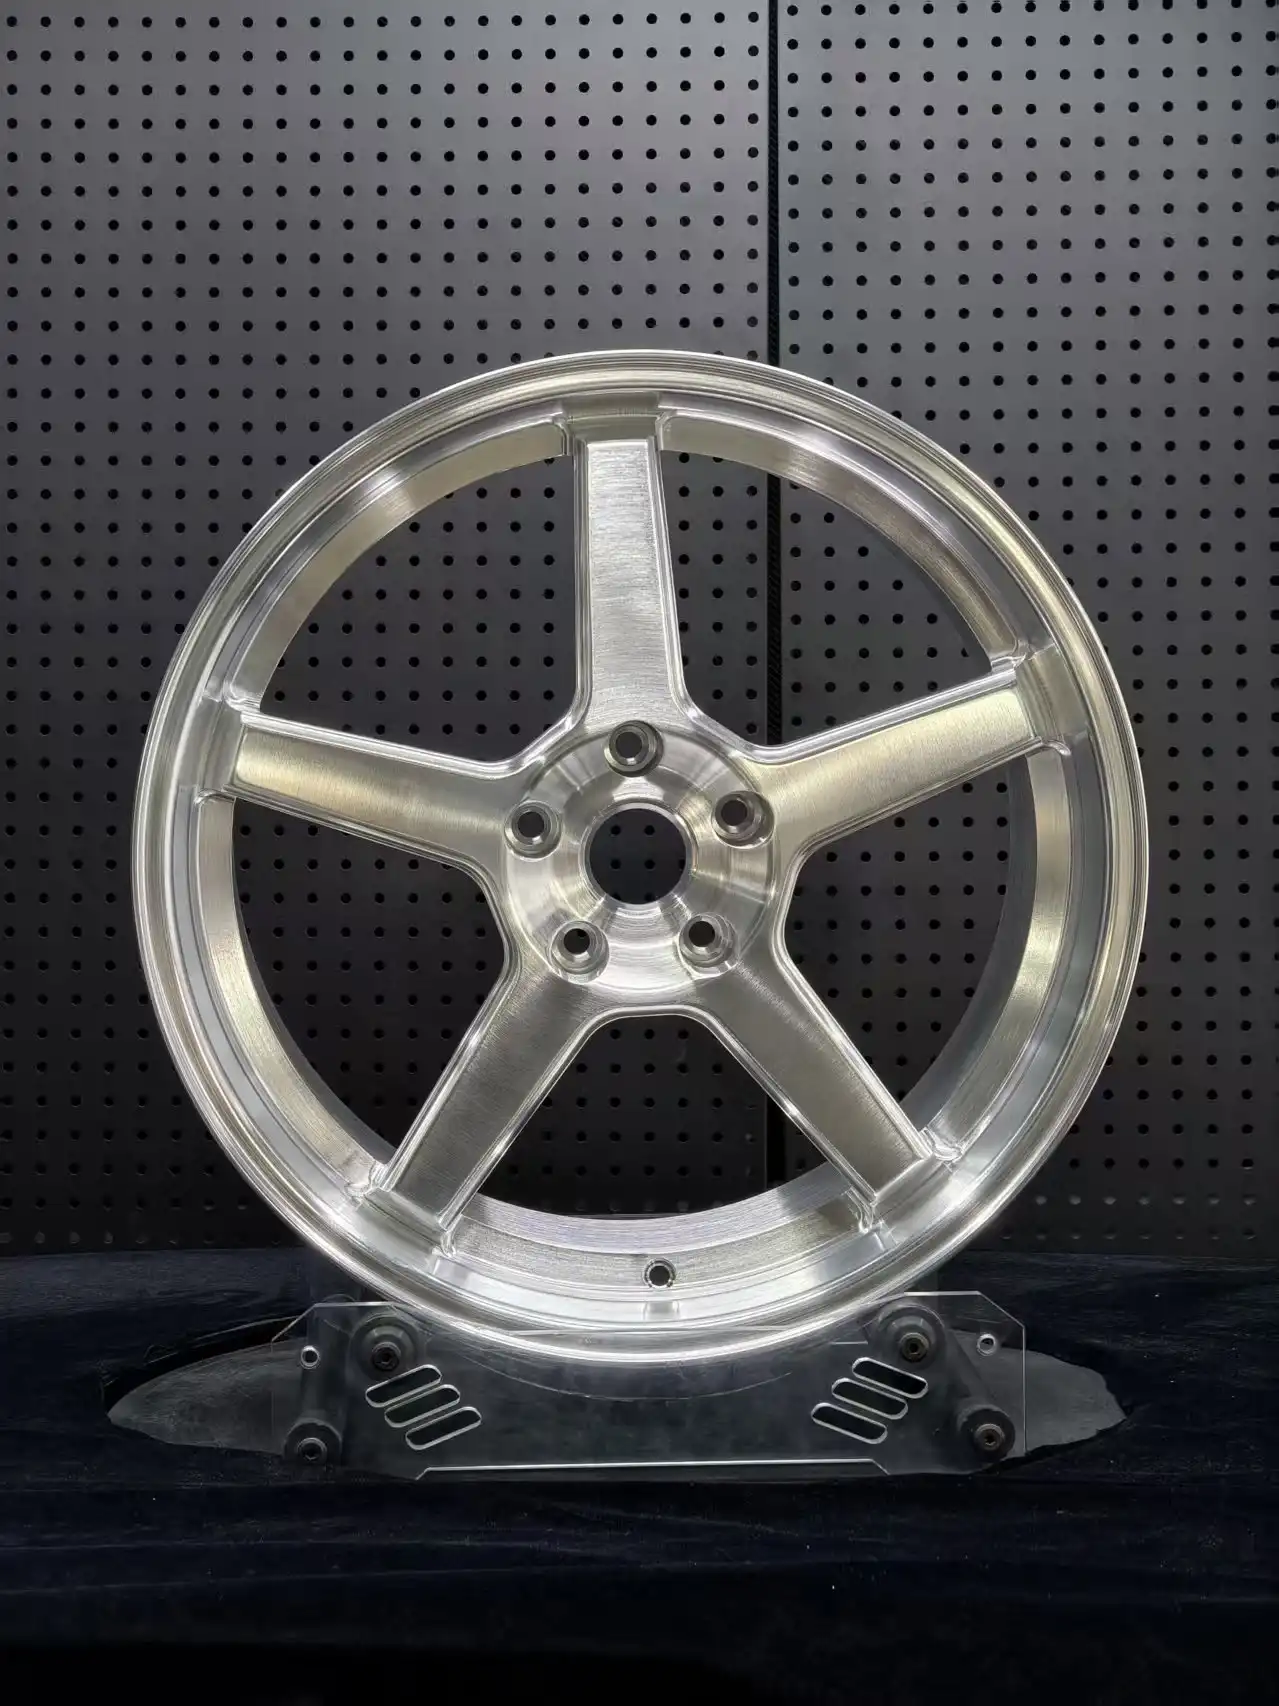
This set was built for a C5-generation Corvette Z06. The specification is a plus-two staggered pair: 19×9.5 at ET43 for the front axle and 20×11 at ET50 for the rear, on a 5×120.65 bolt circle (5×4.75") with a 70.3 mm center bore, weighing 12.6 kg and rated at 800 kg per wheel. The design is a clean five-spoke with broad tapered arms and a flat outer lip. The surface treatment is hand brushing — a finishing process carried out by hand to produce the brushed texture — followed by a transparent protective powder coat that seals the surface for long-term protection without covering the metal.

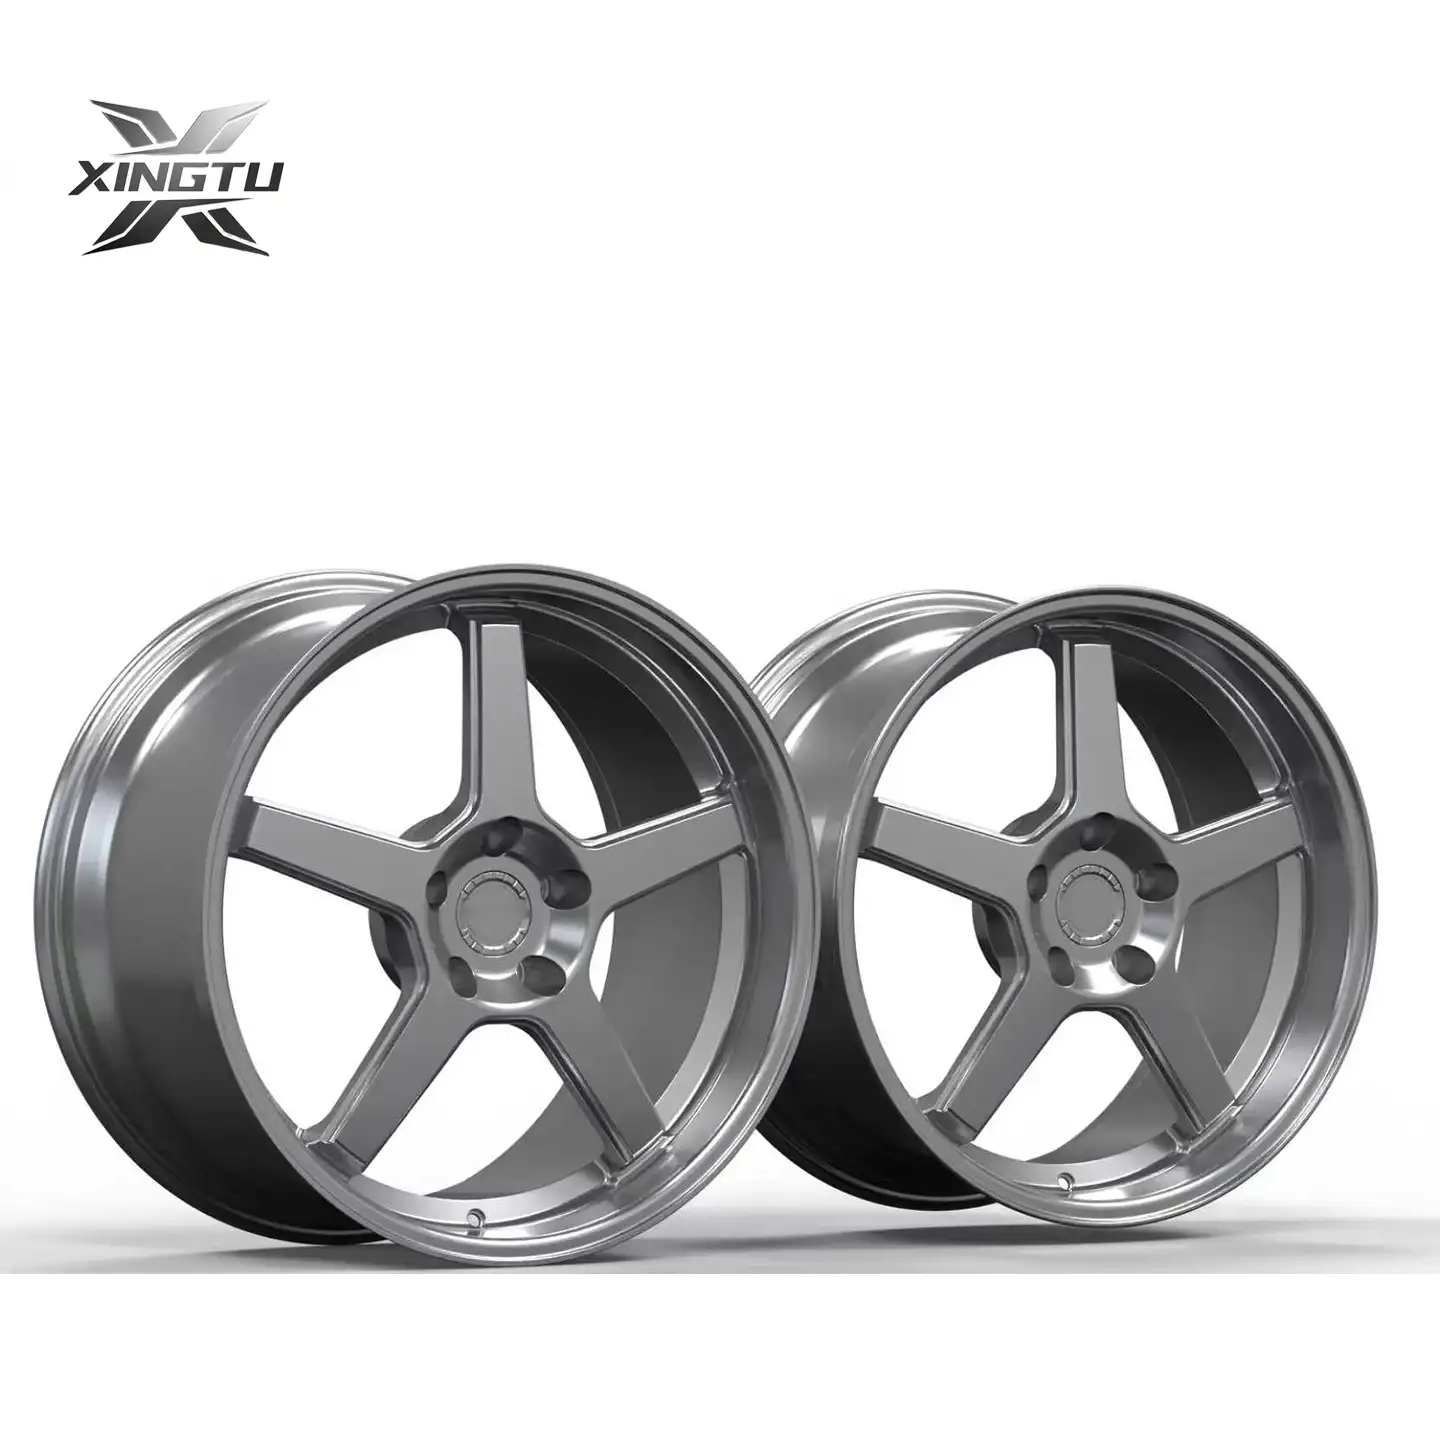
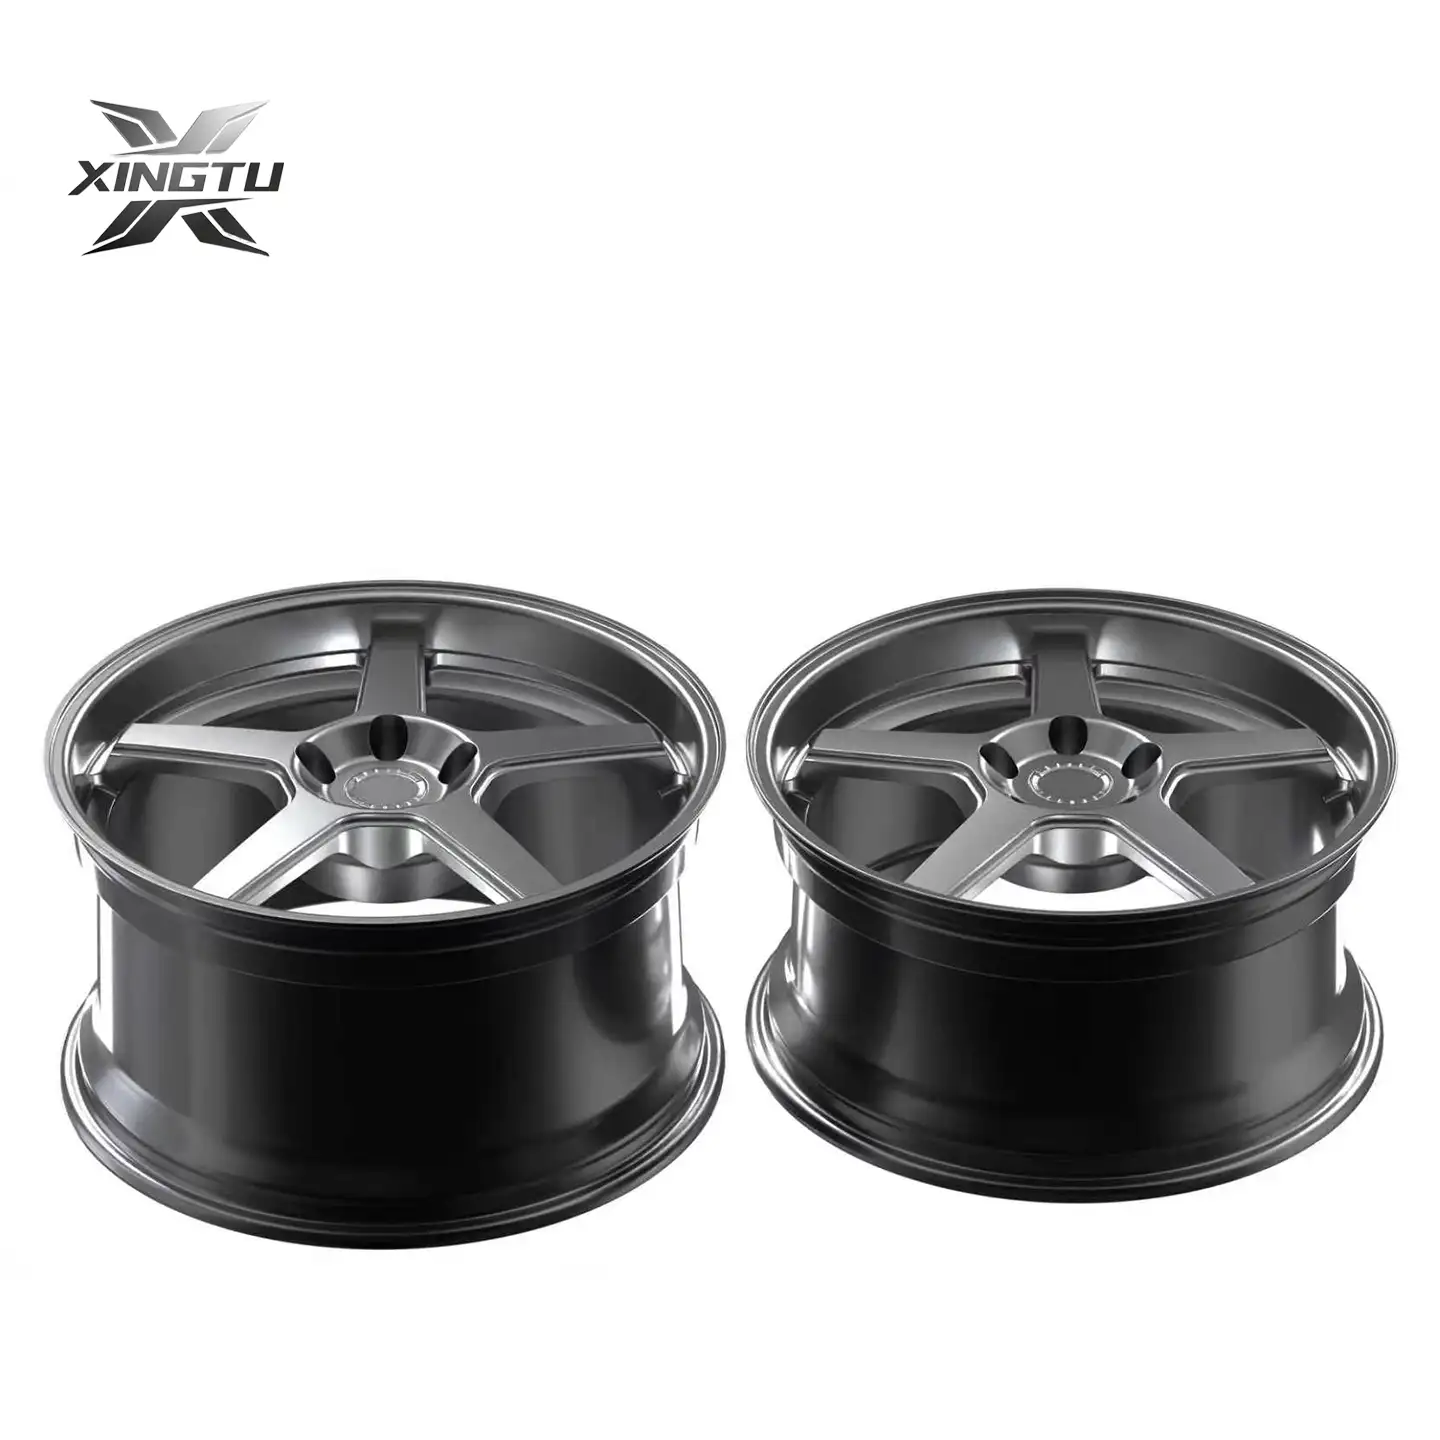


Chevrolet Corvette Z06 (C5) — model year not stated

Forged Monoblock Design

Hand-Brushed Surface + Transparent Protective Powder Coat
Specifications
| Item | Specification |
| Model No. |
L266531 (blank: JC114 / JC023) |
| Size |
Front: 19×9.5 Rear: 20×11 |
| PCD |
5×120.65 (5×4.75") |
| Offset (ET) |
ET43/50 |
| Center Bore |
70.3 mm |
| Weight |
12.6 kg per wheel |
| Load Rating |
800 kg per wheel |
| Lug Seat |
15×32 60° taper |
| Finish |
Hand-Brushed Surface + Transparent Protective Powder Coat |
| Construction | Forged Monoblock |
| Fitment Basis | Check Data |
| Lead Time |
28 days (brushed finish) |
-
Descriptions

XINGTU's engineers want to highlight three details that define this build.
First, the set was built to the submitted data on both axles: 19×9.5 ET43 front and 20×11 ET50 rear, 5×120.65 PCD, 70.3 mm center bore and a 15×32 60° taper seat. The 5×120.65 pattern (5×4.75") and the 70.3 mm bore are consistent with published C5 Corvette data, and the taper seat matches conical-seat hardware, so ball-seat nuts must not be substituted. This is a plus-two set against the factory C5 Z06 fitment of 17×9.5 front and 18×10.5 rear — the front keeps its width but moves roughly 11 mm outboard, while the rear gains half an inch and sits about 12 mm further out at the outer edge with the inner edge essentially unchanged. On a C5 that means checking the front liner, the brake cooling duct and the front transverse leaf spring at full lock, plus the rear inner wheel well at full compression, before the offsets are signed off. The 5×120.65 pattern must never be treated as 5×120: the two differ by 0.65 mm, and that gap is not something an offset or a wobble bolt should absorb. Tire sizing also has to be fixed first, because this set is two inches larger in diameter and the plate gives no tire data.
Second, the construction is a forged monoblock: the five spokes, the hub pad and the full barrel are machined from one continuous forged blank, with no bolted joint. The spokes are broad at the hub pad and taper as they meet the rim, which suits this load path — the arm carries bending through its depth rather than through a thin blade, so the wheel holds 800 kg at 12.6 kg without adding material to the barrel. The flat outer lip is a machined feature of the same forging, not a separate rim half; the wheel is a single structural piece and is neither a two-piece nor a beadlock.
Third, the surface is hand-brushed and then given a transparent protective powder coat, and these two stages are scheduled at the end of the build for good reason. Hand brushing is a surface treatment process: a finishing step carried out by hand to produce the brushed texture, giving the aluminium a fine directional grain that catches light along the spokes and around the lip, and reads as a low-gloss metal rather than a polished or painted surface. Because it is done by hand, the result depends on control rather than on a program — the same direction, the same pressure and the same line density have to be held across the spokes, the flats between them, the lip and the barrel, and the transitions at the spoke roots and lip radius have to be blended so the grain reads as one continuous surface instead of patches. Once the texture is established, a transparent protective powder coat is applied over it. It is transparent so the brushed metal stays visible, and it is there for long-term protection: it seals the surface against moisture, road salt and brake dust, and keeps the finish stable through normal washing and use. Before coating, the lug seat, the hub bore and the bead area are masked — powder baked onto a 60° taper seat changes the seating face and produces a false torque reading, and film in the bead area affects how the tire seats — and the wheel is not machined or re-torqued after the coat is cured.
From Design to Delivery
Quality Verified
- Front 19×9.5 and rear 20×11 dimensions inspected
- ET43 front and ET50 rear offsets checked
- 5×120.65 PCD and 70.3 mm center bore verified
- 15×32 60° taper seat interface checked
- Wheel weight verified at 12.6 kg
- Load rating confirmed at 800 kg per wheel
- Five-spoke geometry, spoke taper and root radii inspected
- Flat lip and flange profile checked
- Hand-brushed texture checked for direction, density and evenness across spokes, windows, lip and barrel
- Brushed texture coverage checked; no missed or overworked areas
- Spoke root and lip radius transitions checked by hand-blend standard
- Lug seat, hub bore and bead area confirmed fully masked before coating
- Transparent powder checked for clarity, film thickness and colour neutrality after cure
- Brushed texture confirmed still visible under the transparent coat
- Powder adhesion checked on coupon and finished part
- Radial and lateral runout checked
- Dynamic balancing completed for every wheel
Result
The finished wheel reads as a hand-finished aluminium wheel that has been properly sealed: the brushed texture runs down each spoke and around the lip, catching light at an angle, and the transparent powder sits over it without tinting the metal or flattening the grain.
That combination is the point—the wheel keeps the honest look of brushed aluminium while the surface is protected against moisture, salt and brake dust, so it stays stable through normal washing and use.
Because the protection is a cured powder layer rather than bare metal, the finish is permanent; it is not spot-repaired the way bare aluminium can be, and a colour change later means stripping the coating rather than painting straight over it.
Building a plus-size set for a C5 and want a hand-brushed metal look that still holds up to weather?
XINGTU develops forged monoblock, two-piece and three-piece wheels around your hub data, brake package, suspension clearance and load target, and can deliver hand-brushed with transparent protective powder, brushed with clear coat, painted or two-tone finishes.
-
Build & Fitment
Plus-Two Upgrade & Mandatory On-Car Check
This is a plus-two upgrade for C5 Z06. Front shifts 11 mm outward, rear extends 12 mm outward with wider barrel. Full vehicle clearance verification is required: front liner, brake duct, leaf spring full-lock clearance and rear wheel well full-compression clearance. Tire size must be confirmed before production.
Premium Hand-Brushed Texture Standard
Entire wheel adopts uniform hand-brushed directional grain. Strict consistency on direction, pressure and density across all surfaces with smooth transition blending, delivering low-gloss raw metal visual effect.
Transparent Powder Coat & Masking Rule
Clear protective powder coat preserves brushed texture and resists corrosion. Lug seat, hub bore and bead area are fully masked during coating to avoid incorrect torque values and poor tire seating. No post-coat machining or retorque.
-
FAQs
1. Can 5×120 bolts or adaptive wobble bolts be used?
5×120.65 and 5×120 are not interchangeable. No offset bolts are permitted for safety.
2. Why is full on-car clearance check necessary?
The plus-two upgraded size pushes wheels further outboard. Front steering lock and rear suspension compression positions must be verified to avoid rubbing.
3. Is this wheel two-piece or beadlock style?
It is pure monoblock forged. The flat lip is one-piece machined cosmetic design.
4. What is the advantage of hand-brushed finish?
Uniform directional metal grain provides premium low-gloss metallic look, more delicate and stable than machine brushing.
5. Why mask seat and bead area during coating?
Powder coating on taper seat causes inaccurate torque; coated bead area affects tire installation and sealing.
6. Production lead time and branding note
The complex brushed process extends the lead time to 45 days. The centre hub remains a blank disc for later cap installation; no external brand emblem will be fitted during factory production.
Related Products